- Home
- About
-
Product
-

NSH-VFD
Transformer Oil Purification Plants
NSH-VFD is a Dual-stage Vacuum System Purifier, which is used for different power transformers and is suitable for all insulation oils. It is used to remove moisture, gasses, particulate matter, etc. High efficient and easy operation. Stationary or mobile design.
More -

NSH-VFD-Series
Transformer Oil Purification Plants
NSH-VFD series is used for different power transformers and is suitable for all insulation oils. It is used to remove moisture, gasses, particulate matter, etc. Customized solutions are acceptable.
More -

NSH-VFD-A
Transformer Oil Purification Plants
NSH-VFD-A is a fully automatic purifier with a dual-stage vacuum system, which is used for different power transformers and is suitable for all insulation oils. It is used to remove moisture, gasses, particulate matter, etc. Customized solutions are acceptable.
More -

NSH-VFD-R
Transformer Oil Purification Plants
NSH-VFD-R is used for renew the aged transformer oils by regeneration and purification plant. It is able to remove sulfurs as well as the moisture, gasses, particulate matter, etc. High efficient and low cost. Stationary or mobile design.
More -

NSH-VF
Transformer Oil Purification Plants
NSH-VF is a basic solution vacuum oil purifier plant, which is budget friendly. It is used for different power transformers and is suitable for all insulation oils. It is used to remove moisture, gasses, particulate matter, etc. High efficient and easy operation. Stationary or mobile design.
More -

NSH-VFD-M
Transformer Oil Purification Plants
NSH-VFD-M is suitable for outdoor maintenance and installation of transformers. Equipped with weatherproof housing and mobile trailer. Used to remove moisture, gas, particles, etc. contained in transformer oil. Custom solutions are acceptable.
More
-

NSH-TF-Z
Turbine Oil Purification Plants
NSH-TF-Z combines the latest innovations in coalescing separation technology and microglass filtration media in one system, using a specially designed filter element that can effectively and quickly separate water and oil, break emulsions, and remove particulate pollutants.
More -

NSH-TF-A
Turbine Oil Purification Plants
NSH-TF-A is a fully automatic purifier with a vacuum system, which is suitable for all turbine oils. It is used to remove moisture, gasses, particulate matter, etc. Customized solutions are acceptable.
More -

NSH-TF-E
Turbine Oil Purification Plants
NSH-TF-E is Explosion-proof type designed for flammable and combustible working conditions in power plant. It is a vacuum purification plant which is used for turbine oils and is able to remove large large water, gasses, particulate matter, etc. Customized solutions are acceptable.
More -

NSH-TF-Series
Turbine Oil Purification Plants
NSH-TF is a vacuum oil purifier plant which is used for turbine oils. It is able to remove large large water, gasses, particulate matter, etc. Customized solutions are acceptable.
More -

NSH-TF-C
Turbine Oil Purification Plants
NSH-TC is a combination plant of vacuum and centrifugal separator, which has a high efficiency of large water and particluate removal. It is suitable for all turbine oils. Customized solutions are acceptable.
More
-

NSH-LV-E
Lubrication Oil Purification Plants
NSH-LV-E is Explosion-proof type designed for flammable and combustible working conditions in power plant. It is a vacuum purification plant which is used for turbine oils and is able to remove large large water, gasses, particulate matter, etc. Customized solutions are acceptable.
More -

NSH-LV
Lubrication Oil Purification Plants
NSH-LV is a vacuum oil purifier plant which is suitable for hydraulic oil. It is able to remove moisture, gasses, particulate matter, etc. Customized solutions are acceptable.
More -

NSH-LV-A
Lubrication Oil Purification Plants
NSH-LV-A is a fully automatic purifier with a vacuum system, which is suitable for all types of lubrication oils, such as hydraulic oil, machine oil, coolant oil, etc. It is used to remove moisture, gasses, particulate matter, etc. Customized solutions are acceptable.
More -

NSH-LV-Series
Lubrication Oil Purification Plants
NSH-LV series oil purifier is suitable for all types of lubrication oils, such as hydraulic oil, machine oil, coolant oil, etc. It is able to remove moisture, gasses, particulate matter, etc. Customized solutions are acceptable.
More
-

NSH-GED-WD
Oil Distillation and Regeneration Plants
NSH-GED-WD is a waste oil distillation system that cracks waste oil to diesel fuel.
More -

NSH-GED-WB
Oil Distillation and Regeneration Plants
NSH-GED-WB is designed to process and recycle waste lubrication oils by vacuum distillation techonology, thereby to acquire high quality base oil.
More -

NSH-GER
Oil Distillation and Regeneration Plants
NSH-GER is designed with the combination technology of physical and chemical processing, can effectively remove aging products and contaminants from aged black engine oils.
More
-

NSH-FV
Flame-resistant Oil Purifier
NSH-FV is specialized for phosphate ester fuel-resistant oil. Adopts advanced hydrophilic and hydrophobic principles, the equipment is stainless steel made and could work for dehydration, de- acidification, broken emulsion, and high precious filtration.
More
-
NSH-CP/CPA/CPPA-E
Centrifugal Separator
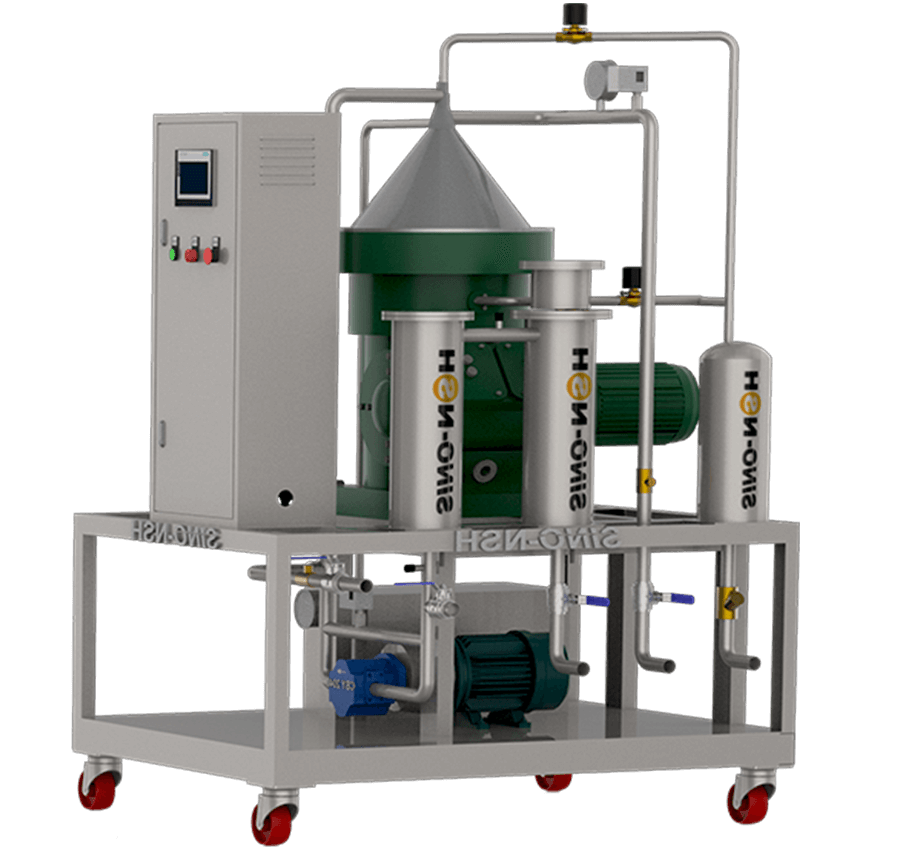
NSH-CP/CPA/CPPA-E is Explosion-proof type designed for flammable and combustible working conditions. It is combination system with thermal, filtering and centrifugal separation processing. Customized solutions are acceptable.
More -

NSH-CP
Centrifugal Separator
NSH-CP series is an oil purification system with thermal, filtering and centrifugal separation processing, with capacity from 1500 liter/hour to 6000 liter/hour.
More -

NSH-CPA-CPPA
Centrifugal Separator
NSH-CPA/CPPA is is a fully automatic ith thermal, filtering and centrifugal separation processing, with capacity from 1500 liter/hour to 6000 liter/hour. Customized solutions are acceptable.
More
-

NSH-VR
Corollary Equipment
NSH-VR is a double-stage vacuum system. Specialized for transformer or other falicities evacuation job. Wide range of capacity. High efficiency, low consumption, easy operation. Customized solutions are acceptable.
More -

NSH-HLC
Corollary Equipment
NSH-HLC is a recycling and charging device for Sulfur Hexafluoride Gas (SF6). It is suitable for on-site installation and maintenance of 110KV ~ 220KV GIS switch and 110KV ~ 800KV GIS switches.
More -

NSH-ADK
Corollary Equipment
NSH-ADK is widely used for various transformer drying applications. It can purge clean, dry air into a confined transformer while maintenance personnel cary out routine repairs.
More -

NSH-LF
Corollary Equipment
NSH-LF is used to remove harmful contaminants for a large oil system,such as hydraulic control systems,rotating equipment lubrication systems,and turbine/generator unit,etc. It will keeps the equipm ent operating at peak performance and reducing the potential for failure.
More
-
- Cases
- News
- Contact

